A356-T6 selective surface finishing
Coordinating pretreatment, selective masking, thread inserts and inspection for an A356-T6 part requiring conversion coating, hard anodizing and paint.
Material and finish requirements
| Material | A356-T6 aluminum alloy |
|---|---|
| Pretreatment | Abrasive blasting |
| Chemical conversion coating | Chemical conversion coating (Alodine) per MIL-DTL-5541, Class 3, clear. |
| Hard anodizing | Black hard anodizing per MIL-A-8625, Type III, Class 2; coating thickness 40 ± 5 µm. |
| Thread inserts | Install Heli-Coil wire thread inserts. |
| Primer painting | Epoxy primer per MIL-PRF-23377J, Type II. |
| Topcoat painting | Polyurethane topcoat per MIL-PRF-85285, color No. 37038 per FED-STD-595; gloss < 2%. |
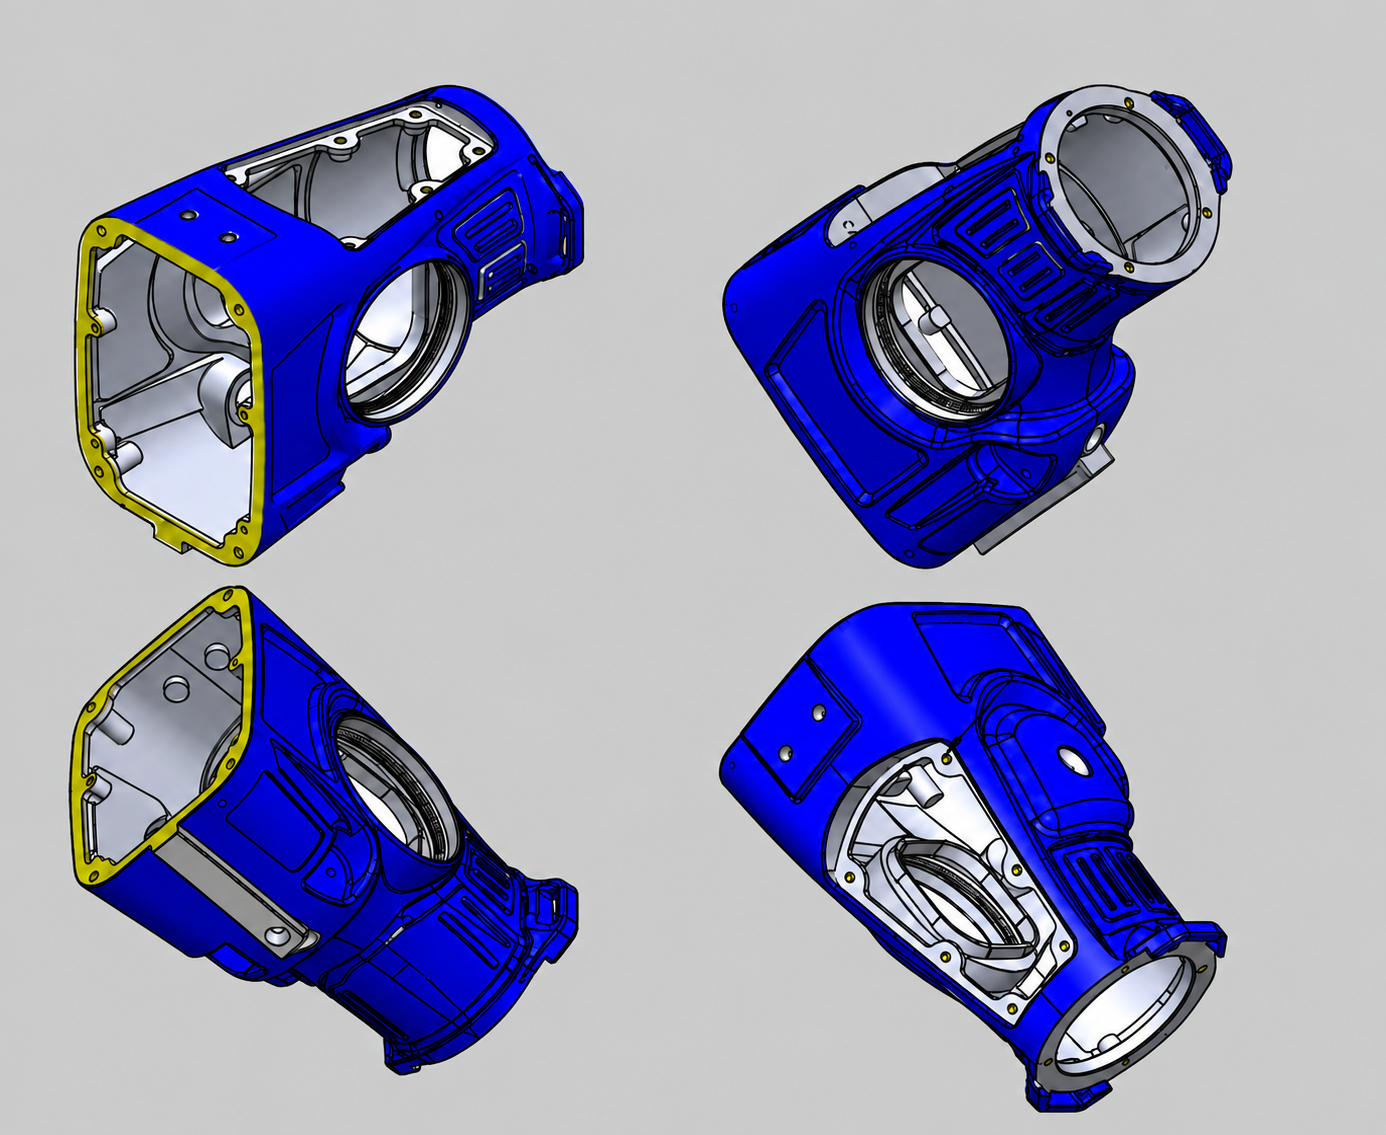
Drawing colors identify treatment zones, not final part colors: yellow for conversion coating, gray for hard anodizing, and blue for painting.
Project finishing sequence
- Abrasive-blast the entire part.
- Apply Alodine chemical conversion coating to the entire part.
- Mask the areas identified in yellow.
- Apply black hard anodizing to the unmasked areas.
- Protect the yellow and gray areas with masking fixtures for painting.
- Install Heli-Coil wire thread inserts.
- Apply the specified primer and polyurethane topcoat only to the blue areas.
- Remove the masking fixtures and masking materials.
- Inspect against the project drawing and agreed acceptance requirements.
This sequence reflects the project’s treatment zones. Execution follows approved drawings and process documents, including the gloss measurement angle and method.